
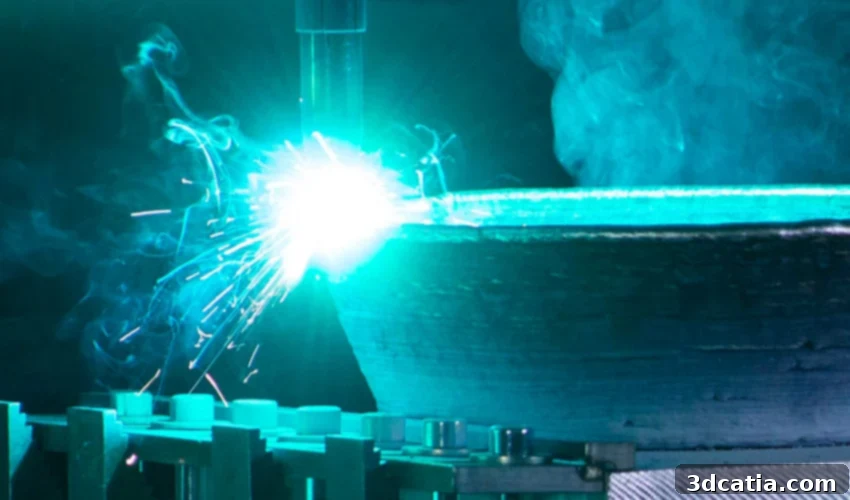
Wire Arc Additive Manufacturing (WAAM): The Definitive Guide to Large-Scale Metal 3D Printing
Wire Arc Additive Manufacturing (WAAM) stands as a prominent and rapidly evolving technology within the realm of Directed Energy Deposition (DED) 3D printing processes. DED is a sophisticated metal additive manufacturing technique that involves precisely depositing material, typically in powder or wire form, onto a substrate using a nozzle mounted on a multi-axis robotic arm. A concentrated energy source, which could be a laser, electron beam, or plasma, then melts the material as it is applied, allowing for the layer-by-layer construction of a part. What distinguishes WAAM within the DED family is its utilization of an electric arc as the primary heat source, a concept directly adapted and refined from conventional arc-welding processes. This innovative approach harnesses the well-understood principles of welding to build intricate and large-scale metal components with significant efficiency.
What is Wire Arc Additive Manufacturing (WAAM)?
At its core, WAAM technology is fundamentally based on established automated welding techniques, integrated with advanced robotic systems to achieve additive layer-by-layer fabrication. Common welding processes that form the basis of WAAM include Metal-Inert Gas (MIG) or Metal-Active Gas (MAG) welding, Tungsten-Inert Gas (TIG) welding, and Plasma Arc-Wire (PAW) welding. Each of these methods offers specific advantages regarding material deposition rates, heat input control, and overall process stability. Furthermore, specialized variations like the Cold Metal Transfer (CMT) welding process, pioneered by Fronius in 2004 and derived from MIG welding, are also employed in WAAM to achieve lower heat input and enhanced material transfer control. This versatility in welding techniques allows WAAM to be compatible with a broad spectrum of metals. These include high-performance alloys such as titanium, known for its exceptional strength-to-weight ratio in aerospace applications; aluminum, valued for its lightweight properties; durable nickel alloys, often used in high-temperature environments; and various steel alloys, which provide robust and cost-effective solutions for many industrial requirements. The ability to work with such a diverse range of engineering metals positions WAAM as a highly adaptable solution for complex industrial demands.
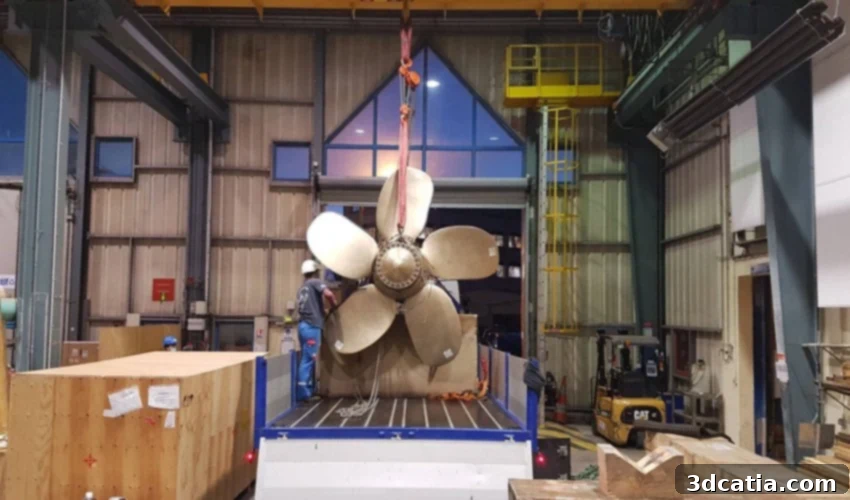
A 3D-printed propeller by Naval Group, showcasing the large-scale capabilities of WAAM (photo credits: Naval Group)
Diverse Applications of WAAM 3D Printing
Much like other DED processes, WAAM is extensively utilized for the repair of expensive industrial equipment and the reproduction of legacy parts that are no longer manufactured, thereby ensuring the longevity and operational continuity of older machinery. However, the capabilities of WAAM extend far beyond mere repair; the technology is increasingly employed for the direct manufacturing of entirely new and complete components. WAAM has found significant traction across a multitude of critical industrial sectors, including aeronautics, aerospace, automotive, energy, and defense. Within these industries, it is leveraged for the rapid production of prototypes, the fabrication of custom molds, the creation of unique single parts, and the efficient manufacturing of small-batch series. While its widespread adoption for mass production is still undergoing rigorous evaluation, WAAM is exceptionally well-suited for the creation of large, structurally significant metal parts, where its speed and material efficiency offer distinct advantages over traditional manufacturing methods.
Real-World Examples: WAAM in Action Across Industries
The practical implementation of WAAM technology is illustrated by numerous compelling examples across various high-stakes sectors. In the maritime and defense sectors, Naval Group famously employed WAAM to manufacture a substantial propeller for the mine-hunting ship Andromède. This showcases WAAM’s ability to produce large, complex, load-bearing components with critical performance requirements. In the energy sector, Vallourec utilized WAAM to produce the first sealing ring designed to enhance the safety and operational integrity of EDF Hydro’s hydroelectric installations. This particular component measured an impressive one meter in diameter and weighed 100 kg, demonstrating WAAM’s capacity for creating large, heavy-duty parts vital for industrial infrastructure. The robotics and construction industries have also embraced WAAM; MX3D, for instance, famously employed the technology to construct a fully functional steel bridge in Amsterdam, pushing the boundaries of what is achievable with additive manufacturing. MX3D has also applied WAAM to produce structural steel connectors, pipe connectors for the demanding oil and gas industry, as well as complex gears and custom components tailored for large-scale industrial machinery. More recently, in the aerospace domain, Relativity Space has leveraged this technology to construct significant portions of its Terran 1 light launcher, highlighting WAAM’s potential for manufacturing critical, large-scale rocket components with speed and efficiency. Additionally, the production of molds for the plastics industry remains a common and highly effective application, where WAAM’s ability to create robust tooling quickly offers significant advantages.
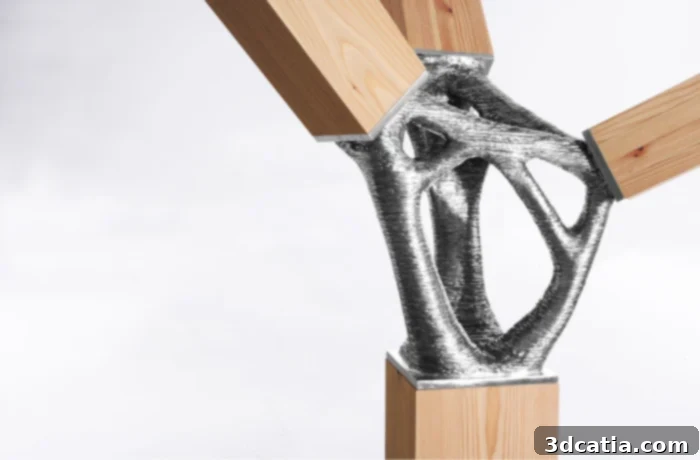
The Takenaka steel connector from one of Japan’s leading architectural firms, produced with MX3D’s WAAM technology (photo credits: MX3D)
Key Advantages of WAAM Technology
Wire Arc Additive Manufacturing offers a compelling suite of advantages that position it as a highly attractive solution for specific industrial applications. Firstly, its inherent high printing speeds represent a significant benefit, drastically reducing production times and accelerating the journey from design to finished part. This speed translates into faster time-to-market and increased agility in manufacturing workflows. Secondly, the overall operational costs associated with WAAM systems are notably lower compared to machines employing powder-bed fusion technologies, such as Selective Laser Melting (SLM). This cost efficiency stems from several factors, including the lower price of wire feedstock compared to metal powders, and often, simpler and less energy-intensive equipment requirements. Thirdly, WAAM technology uniquely excels in its capacity to produce extremely large metal parts. Unlike other additive manufacturing methods that are limited by build volume, WAAM can construct components measuring several meters in dimension, making it ideal for industries requiring colossal structures. Finally, as previously mentioned, WAAM boasts compatibility with an extensive array of engineering metals and alloys. This broad material palette provides manufacturers with immense flexibility, allowing them to select the optimal material for specific mechanical properties, environmental resistance, and cost considerations, further expanding the versatility of the technology.
Understanding the Limitations of WAAM
Despite its numerous benefits, the WAAM process is not without its limitations, which are important to acknowledge for appropriate application. A primary trade-off for its faster printing speeds is a comparatively lower level of detail and dimensional accuracy when contrasted with high-precision powder-bed fusion technologies. While WAAM excels at creating large structures, achieving intricate geometries or very fine surface finishes typically requires subsequent post-processing. Parts manufactured using WAAM technology can also be susceptible to certain defects, such as internal porosities. These porosities, which are small voids or gas pockets within the material, can compromise the mechanical properties of the part, potentially leading to premature failure under static loads or, more critically, reducing fatigue life when the part is subjected to repeated stresses and forces over time. This susceptibility to porosity is particularly pronounced in aluminum parts, which require careful process control to minimize such flaws.
Addressing Residual Stresses and Deformations
Another significant challenge frequently encountered with WAAM technology is the occurrence of residual stresses. These internal stresses arise primarily from the rapid heating and cooling cycles inherent in the arc welding process, leading to uneven thermal expansion and contraction within the deposited layers. Unmanaged residual stresses can manifest as undesirable deformations in the part’s dimensions and/or overall shape. Common examples include curling (the upward bending of edges), warping (distortion of flat surfaces), or even delamination (the separation of layers). These phenomena are characterized by physical deformation across the layers of the printed part, affecting either the top, bottom, or, in the case of delamination, the integrity of multiple layers throughout the build. Such deformations are a direct consequence of the very high working temperatures and the specific thermomechanical properties of the materials being processed. Ultimately, these structural anomalies can severely impair the part’s ability to withstand exerted forces, potentially leading to functional failure if not properly addressed.
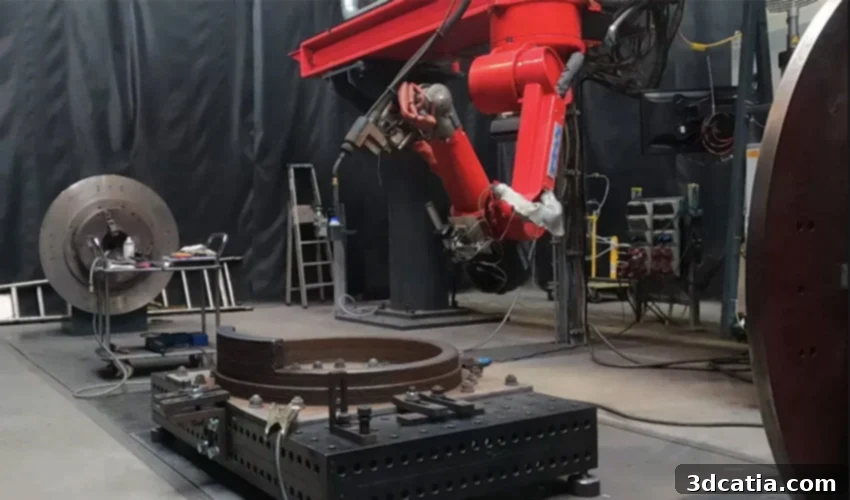
Vallourec leverages WAAM technology for critical components in power plants (photo credits: Vallourec)
Strategies for Mitigating WAAM Defects
To effectively limit the occurrence and severity of these inherent defects, a thorough understanding and precise control of all WAAM process parameters are absolutely crucial. Meticulous adjustment of these parameters ensures a consistent molten metal deposit and a stable heat input throughout the build process. Essential factors that directly influence the quality of the final part include the unwinding speed of the wire, the robotic arm’s feed speed, the welding current, voltage, the layer thickness, the flow rate of the protective shielding gas, and the precise spacing between individual weld beads. Optimizing these variables is paramount for achieving a smooth, defect-free process and robust part integrity. Beyond precise parameter control, technical solutions exist to actively mitigate these anomalies. One effective method is mechanical work-hardening, often achieved through processes like rolling. This technique involves exerting localized pressure on the solidifying weld bead with a roller during the cooling phase. This mechanical compression helps to densify the material, reduce internal porosity, and refine the grain structure. To counteract residual stresses, preheating the base material or subsequent layers before deposition can significantly reduce thermal gradients, thereby minimizing stress accumulation and deformation. It’s also worth noting that certain materials and alloys exhibit greater susceptibility to cracking or delamination than others; for instance, aluminum-copper, aluminum-titanium, and aluminum-iron alloys often require even more stringent process control and specialized mitigation strategies due to their metallurgical characteristics.
Essential Post-Processing for WAAM Components
As with most additive manufacturing technologies, WAAM components typically necessitate a significant amount of finishing post-processing to achieve the desired dimensional accuracy, surface finish, and mechanical properties. This post-processing is generally carried out using conventional machining processes, such as milling or turning, to remove excess material and achieve precise tolerances. In some advanced WAAM applications, an integrated approach is adopted where machining can be performed during the printing phase itself. This is often accomplished by incorporating a second robotic arm equipped with machining tools that can work in tandem with the deposition robot, trimming and shaping the part as it is being built. This “hybrid” manufacturing approach can significantly reduce overall production time and minimize the amount of material that needs to be removed in final finishing steps, streamlining the entire fabrication process.
Leading Manufacturers of WAAM 3D Printers
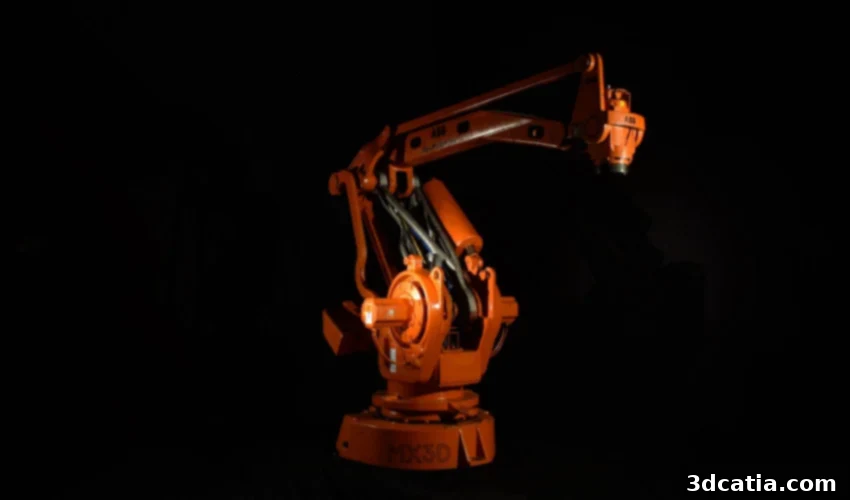
An MX3D 3D printer utilizing advanced WAAM technology for industrial applications (photo credits: MX3D)
The landscape of Wire Arc Additive Manufacturing is populated by a growing number of innovative manufacturers dedicated to advancing this robust technology. Prominent players in this field include Prodways, known for its WAAM-TIG process printers, which offer precision and control; Norsk Titanium, a pioneer with its proprietary Rapid Plasma Deposition (RPD™) process, enabling high-quality titanium components; GEFERTEC, specializing in 3DMP® (3D Metal Print) technology; MX3D, famous for its large-scale architectural and industrial applications; WAAM3D, a dedicated WAAM solution provider; and Lincoln Electric, a long-standing leader in welding technology that has extended its expertise into additive manufacturing. These companies are continually pushing the boundaries of WAAM, expanding its capabilities and making it more accessible for industrial adoption.
What are your thoughts on the transformative potential of WAAM technology for large-scale metal fabrication? We encourage you to share your insights in a comment below or connect with us on our LinkedIn, Facebook, and Twitter pages! Don’t forget to sign up for our free weekly Newsletter here to get the latest 3D printing news delivered straight to your inbox! You can also find all our compelling videos on our YouTube channel.
*Cover Photo: Relativity Space’s Terran 1 rocket under construction (photo credits: Relativity Space)